 مورد مرشح المقصورة HC-Air
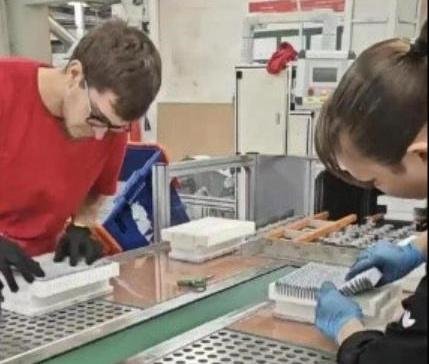
The US client runs a 40,000 sq ft filter plant in Ohio serving the Midwest aftermarket and a nearby light-vehicle OEM line. With cabin filters taking ~55% of US automotive filter revenue in 2025 and HEPA/antiviral variants growing fastest, they needed to shift from manual framing to automated production on charcoal and nanofiber media. Their old semi-auto cell used 7 operators and saw 3–5% edge-band reject in summer AC season. RFQ requirements: 480 V / 60 Hz, NRTL-recognized electrical design, English HMI, <30 min changeover between Ford F-150, Chevrolet Silverado and Toyota RAV4 sizes.
2. Solution & On-Site FAT
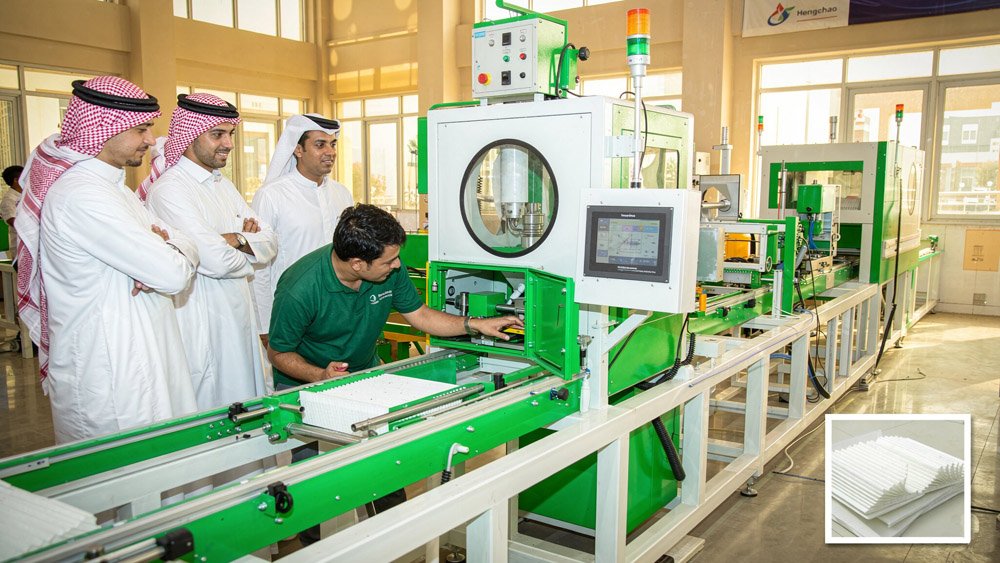
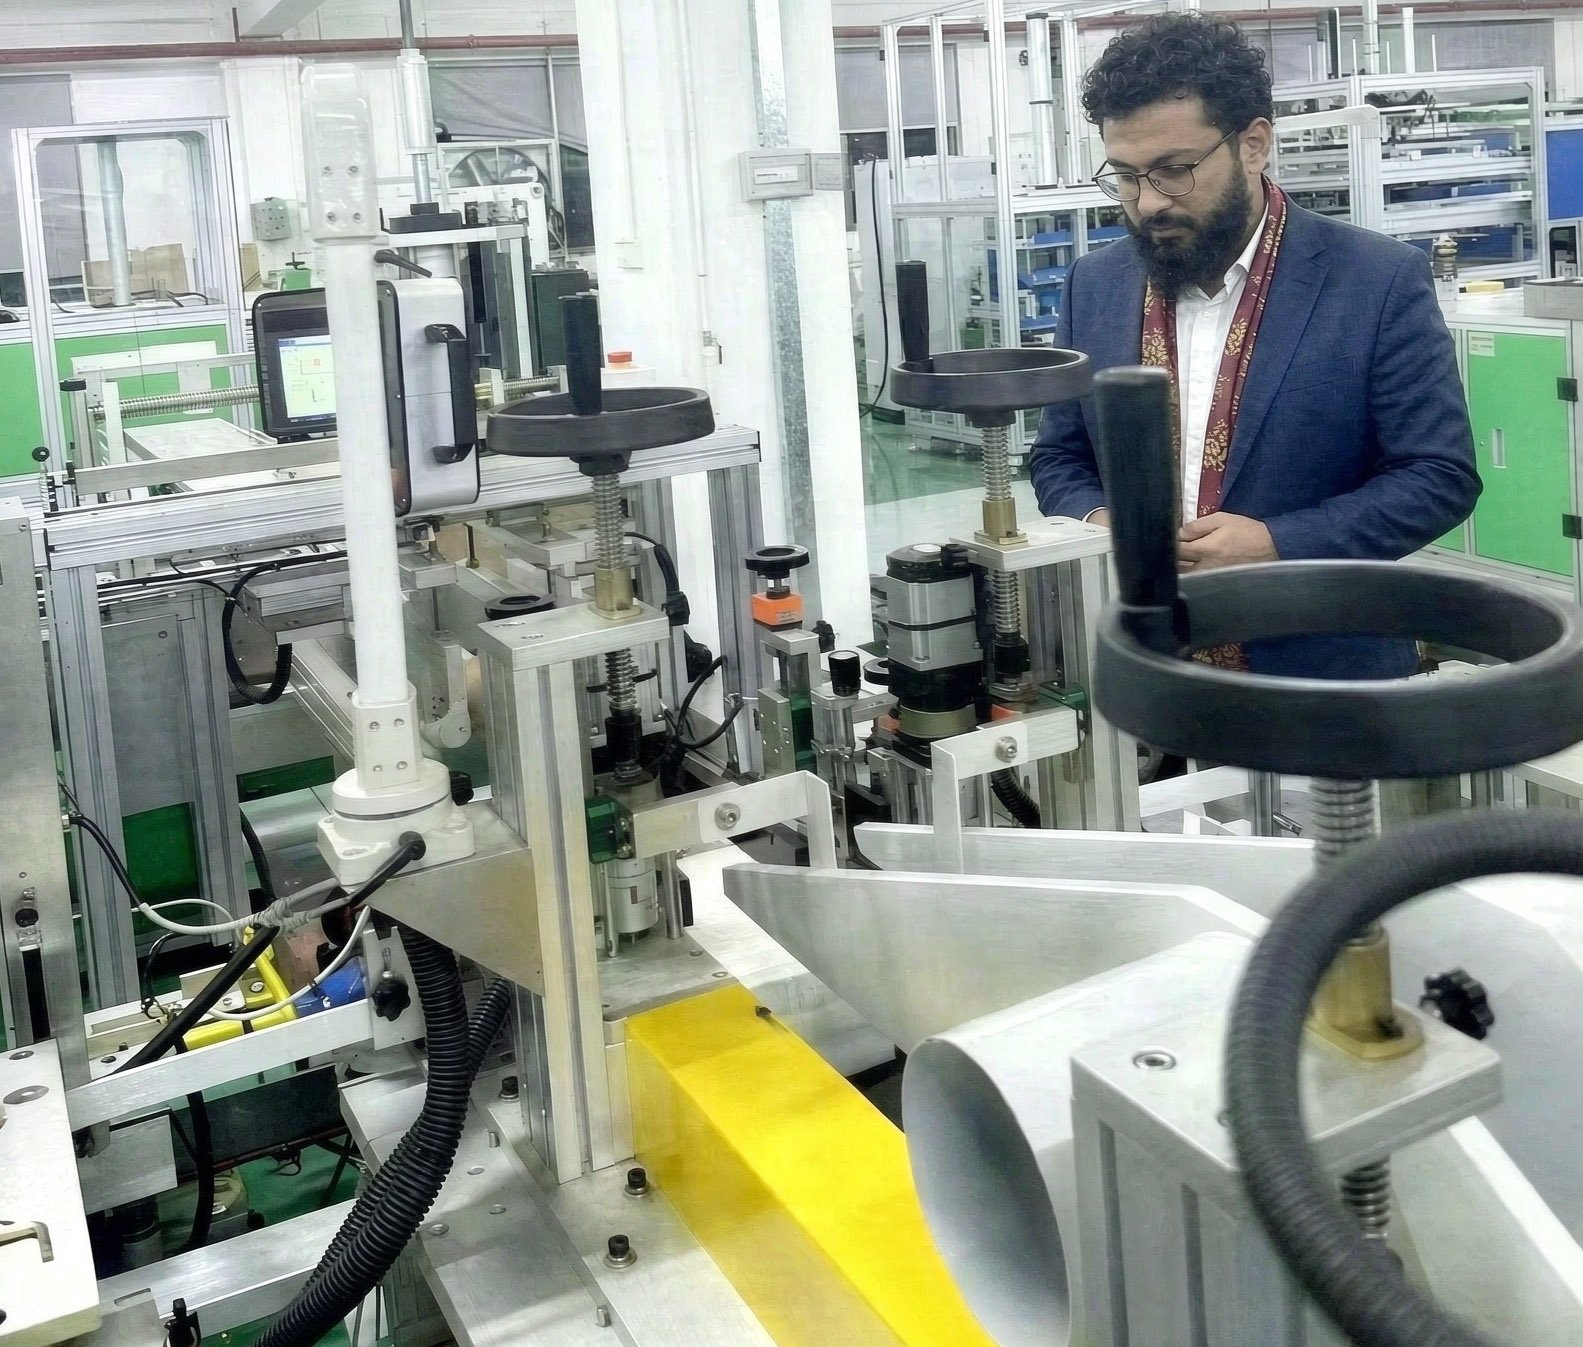
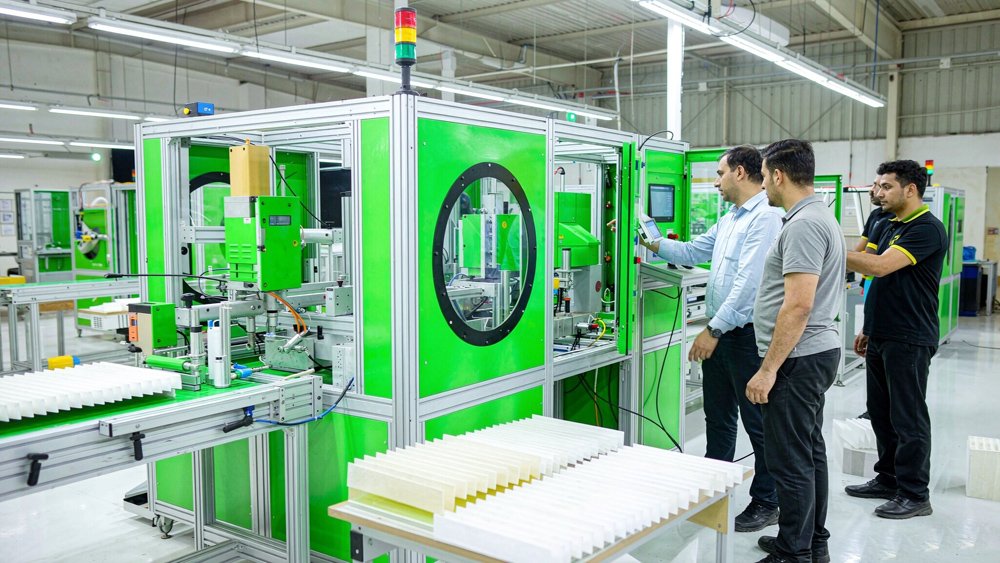
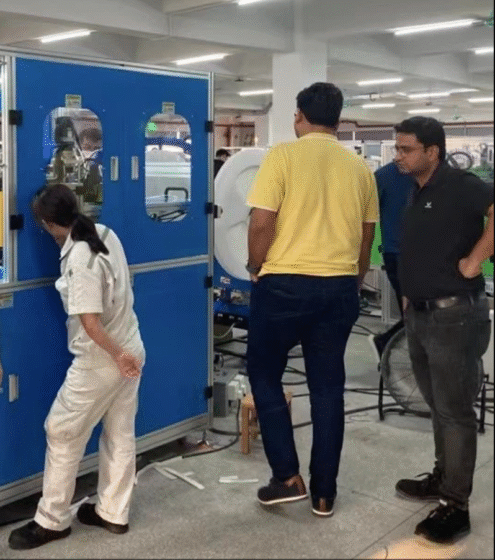
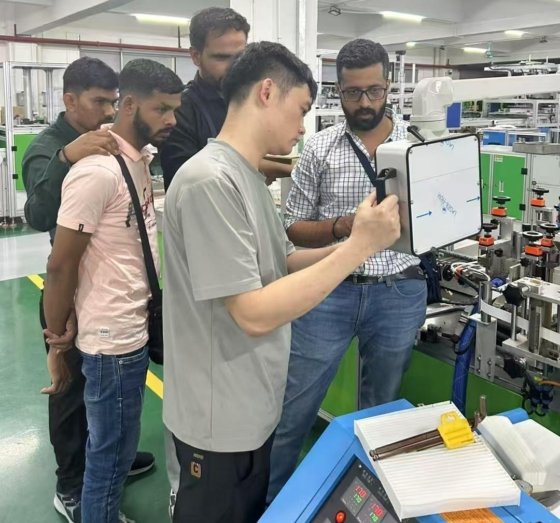
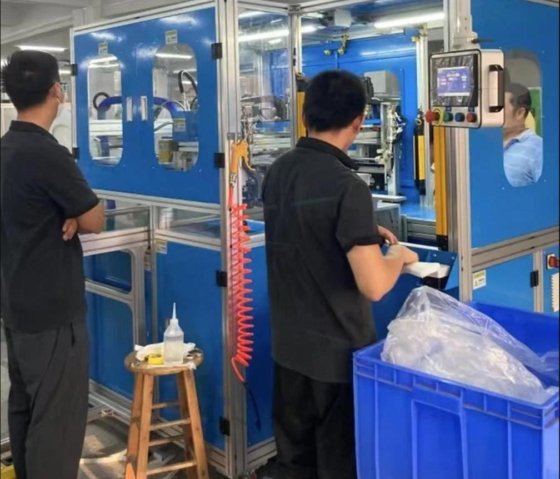
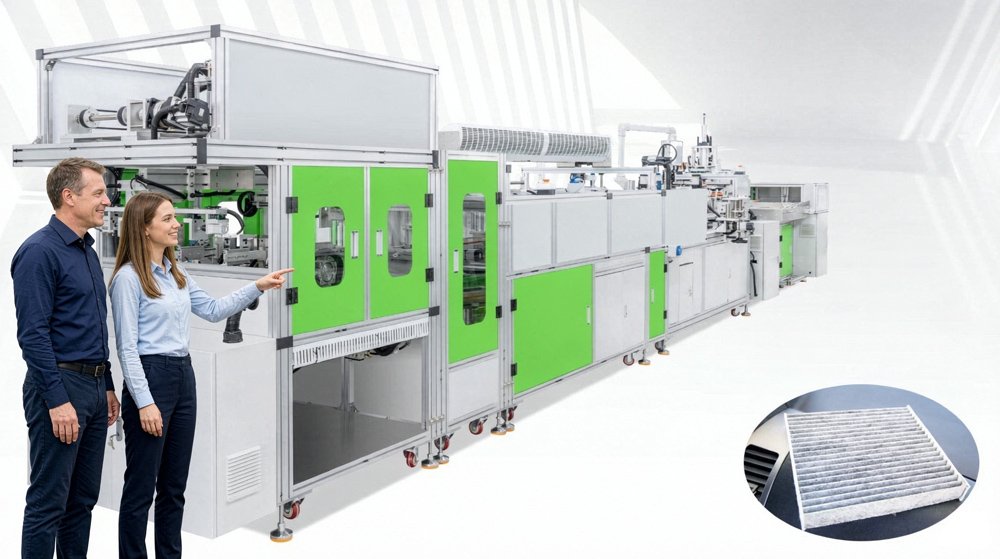
We built a green-and-white aluminum-framed cabin filter machine line. During FAT, two American engineers stood beside the enclosure while our technician tuned the glue head through the circular window:
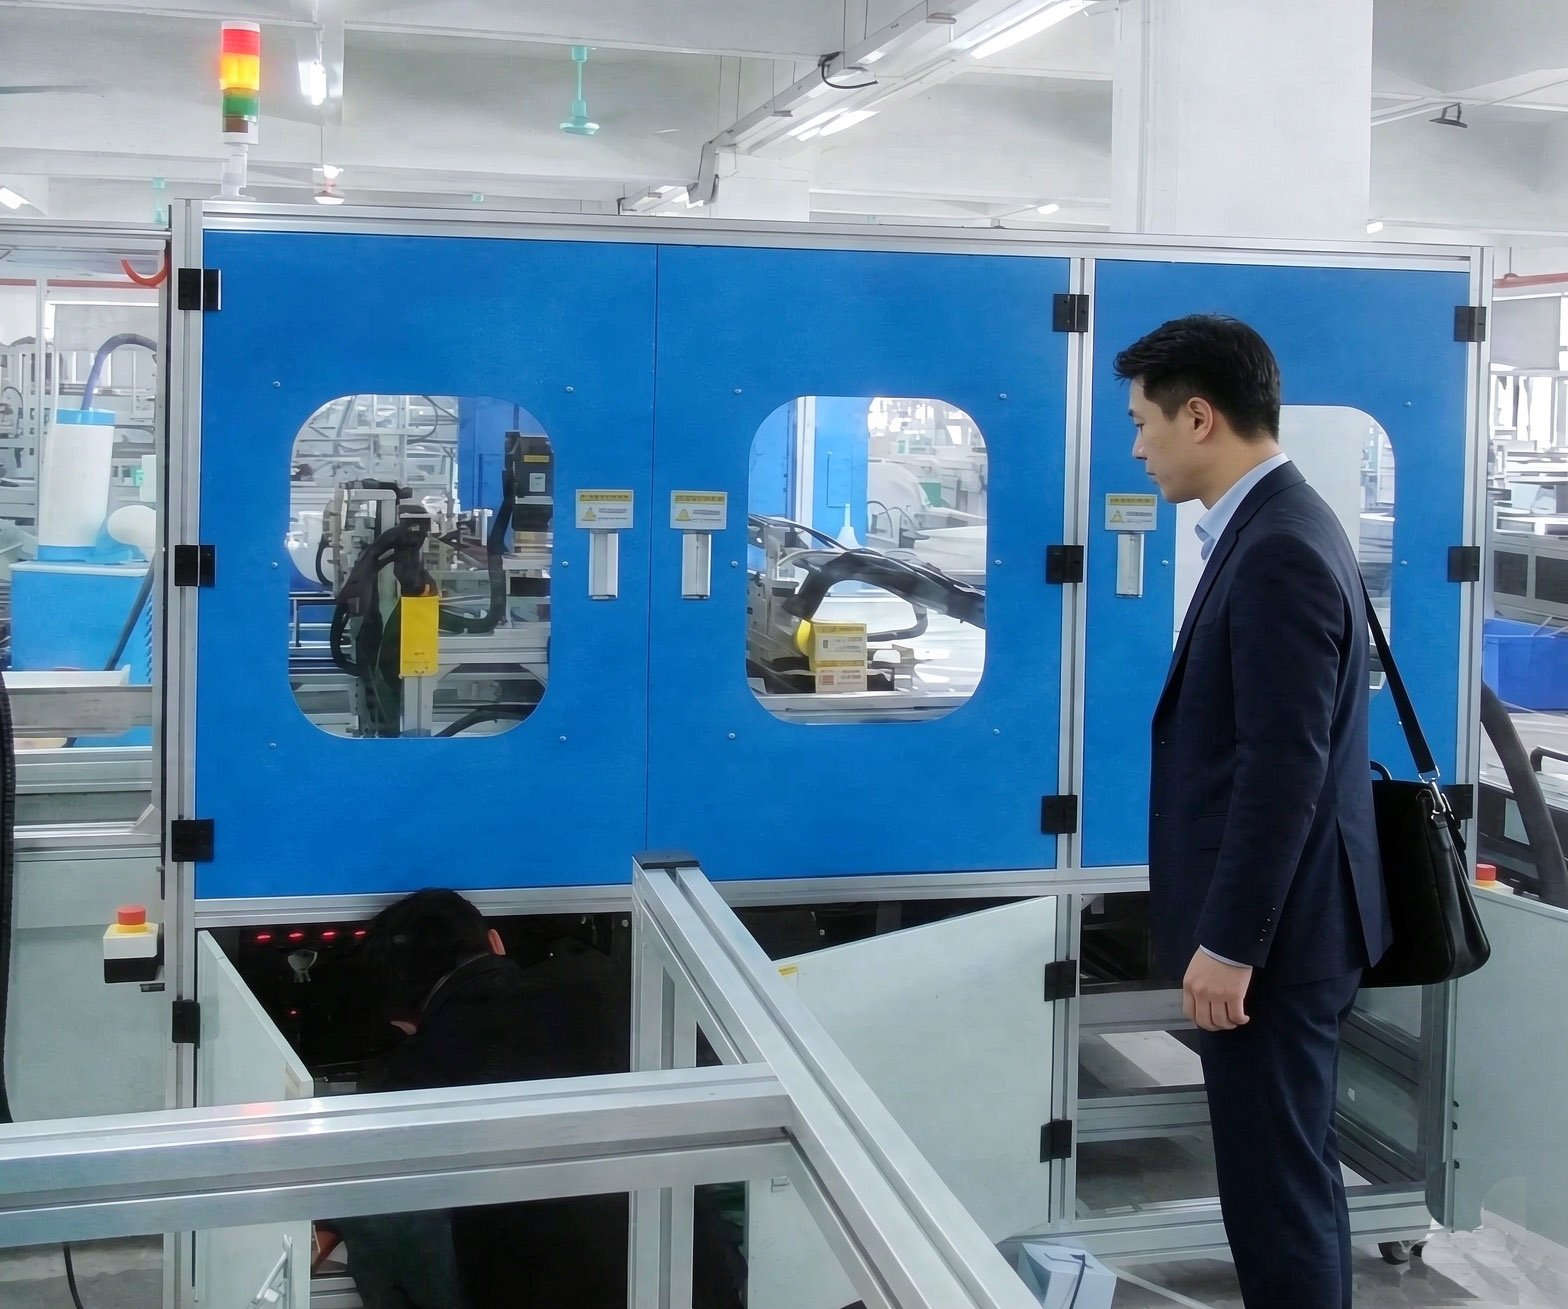
Enclosure & safety: Green doors, circular viewport, stack light, ANSI B11-compliant guards, e-stop, NRTL-ready control panel (UL 508A design basis, components listed; final field label via client’s local AHJ).
Live run: 300 × 280 mm charcoal cabin filter, cycle ≤ 7 s/pc, white trim scraps on floor confirming blade accuracy.
Media handling: Auto tension pleating for paper, non-woven, HEPA/nanofiber and 2-layer charcoal; hot-melt spray/bead switchable.
Electrical: 480 V 3Φ 60 Hz main, 120 V control step-down, NEMA 12 panels, FCC Part 15 EMC consideration.
3. Cooperation Process
Pre-FAT: Client shipped media rolls (standard + activated charcoal + HEPA/nanofiber blend); we ran 600 pcs, shared Cpk and edge-offset data.
FAT week: Ohio team on site, verified 91% OEE, English HMI, inch-unit display, 28-min changeover F-150 ↔ RAV4.
Compliance pack: NRTL component list (UL/CSA/ETL), wiring diagram, OSHA guard checklist, spare-parts kit, PLC backup.
Commissioning: Shipped to Ohio, 6-day on-site startup, operator training on pleat tension, glue temp, mold change, vision reject reset.
4. Results
Operators/shift: 7 → 2 (one feed, one pack/QA)
Reject rate: 4.1% → 0.7% (edge band + trim)
Output: ~500 pcs/h sustained
Changeover: 28 min across Detroit Big Three + Japanese crossover sizes
Tariff angle: Client cited 2025 import-cost pressure as reason to automate domestically instead of buying imported finished filters
“We stood next to the machine for two days during FAT. The green enclosure, the window, the trim scrap on the floor — it proved the line does what the quote says. 480 V wiring and English HMI were drop-in for our plant.”
— Plant Manager, US Client
5. Follow-up
After 5 months running charcoal + HEPA private-label SKUs, client issued PO #2 for a rotary pleater to retrofit Line 2, and requested a quote for BEV thermal-management cabin frame module (2027 program).
العلامات: #CabinFilterMachine #USClient #FAT #Ohio #FilterProductionLine #480V60Hz #NRTL #Automation
LinkedIn short post
🚀 FAT done for our Ohio, USA client — Automatic Cabin Filter Machine.
🇺🇸 480 V / 60 Hz, NRTL-ready panel, English HMI
🔹 Live run on charcoal + HEPA media
🔹 7 s cycle, 0.7% reject, 28-min changeover
🔹 Client engineers beside the green-and-white line, our tech tuning through the round window
Exactly what a Midwest aftermarket+OE supplier needed. Next: rotary pleater PO. #CabinFilter #USA #FilterMachine #FAT